
A cracked cast iron part does not have to be scrapped. CRS Group repairs cracked cast iron housings, machine frames, gearbox casings, manifolds and other castings in Durban, in our Mayville workshop or in position on site, and has done so since 1977.
Call 031 209 3168 or WhatsApp a photo of the crack to 084 511 5929.

Cast iron parts we repair
- Machine beds, frames and pedestals: lathe beds, press frames, mill housings
- Stamping presses, brake presses and injection moulding machines
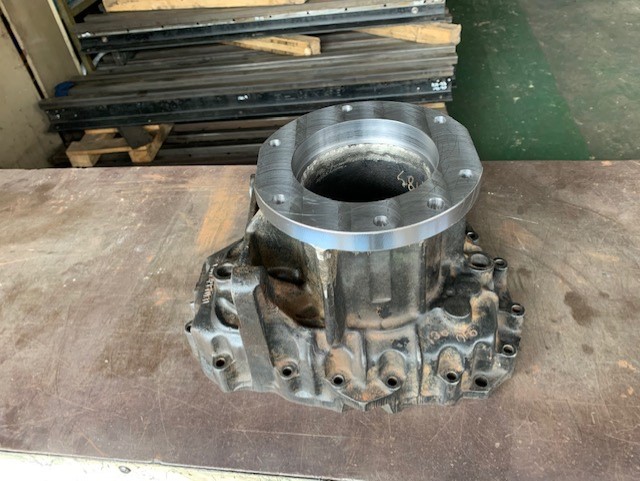
- Gearbox and transmission housings, including resleeving of worn bearing landings
- Pump and compressor casings and end covers
- Exhaust and inlet manifolds
- Crusher and mill frames, jaw stocks and housings
- Moulds, including large moulds
- Marine castings and bedplates
- Obsolete castings that can no longer be bought new
Engine blocks and cylinder heads have their own page: cracked engine block repair.
Why cracked cast iron needs a specialist
Cast iron is strong but brittle. Ordinary welding puts intense local heat into the casting, and as it cools the metal beside the weld becomes harder and more brittle. That is why a welded cast iron part so often cracks again right next to the repair. Fixing it properly means choosing the method to suit the casting, not the other way round.
Two ways we repair cast iron
Metal stitching (cold repair)
For most cracked cast iron this is our first choice. Keys and overlapping pins are fitted across and along the crack with no heat at all, so there is no distortion and no new stress in the casting. It can be done in hazardous areas where a flame or sparks are not allowed, and often without dismantling the machine. Read how it works on our metal stitching page.
Specialised welding
Where material has to be rebuilt, or the section is too thin to stitch, welding is the better answer. We use the correct process with controlled pre-heat and cooling. See specialised welding, or aluminium welding if the part is aluminium and not cast iron.
We will tell you which method suits your part, and why, when we quote.

In our workshop or on your site
Parts that can be moved come to our workshop at 16 Saxon Avenue, Mayville, where the repair can be machined back to size in the same shop. Large castings and installed machines can often be repaired in position, which avoids stripping the machine and cuts downtime. See on-site metal stitching.
Where the part allows it, repairs are pressure tested in the workshop. Some parts are sent to an outside NDT specialist, and repairs done in position on site cannot always be pressure tested.
Repair or replace?
Repairing a casting usually costs well below replacing it, and for an obsolete machine there may be no replacement to buy. A repair also saves the wait for a new casting. Not every part can be saved: if replacement is the better option we will say so before you spend money.
Questions we get asked
Can cracked cast iron be repaired?
In most cases, yes. The method depends on the casting, where the crack is and what the part has to do.
Is it better to weld or stitch cast iron?
For most cracks, stitching, because it adds no heat. Welding is used where material must be rebuilt or the section is too thin to stitch.
Will the repair last?
A correct repair is permanent and should last the working life of the casting. If the crack had a cause, such as misalignment, an out-of-balance rotor or thermal shock, that cause has to be fixed as well or the casting can crack again.
What does it cost and how long does it take?
Both depend on crack length, section thickness, access and whether the work is done in the workshop or on site, so every job is quoted individually. Photos and rough dimensions are enough to start.
Do you only work in Durban?
No. We repair castings across KwaZulu-Natal and South Africa, on site or in our Durban workshop, and smaller parts can be sent to us by courier.
Get a quote
- Phone: 031 209 3168
- WhatsApp: 084 511 5929
- Email: info@crsgroup.co.za
- Address: 16 Saxon Avenue, Mayville, Durban, 4058
- Hours: Monday to Thursday 7:00–15:30, Friday 7:00–14:30