
Worn, cracked or obsolete pump impellers repaired, re-machined or made new in cast iron, bronze and stainless steel. CRS Group has manufactured and repaired impellers for refineries, mills and industrial plant from its Durban workshop since 1977.
Repair or replace an impeller?
An impeller is the hardest-working part of a pump and usually the first to wear. Cavitation pits the vanes, abrasive slurry thins the leading edges, corrosion opens up the shroud, and a stray bolt or stone can crack a vane outright. For a common pump with a dealer in town, a new impeller is the obvious answer. The decision gets harder when the pump is old, imported, out of production, or one of a kind: a replacement impeller can take months to arrive, if the manufacturer still makes it at all, and the pump may be critical to a process that cannot wait.
CRS Group offers three routes. Repair the existing impeller where the damage is local. Machine it back to specification where wear has taken it out of tolerance. Or manufacture a new one, reverse-engineered from your worn sample or made from drawings, in the material the duty calls for.
Impeller repair
Local damage is repaired by welding and machining. Pitted and eroded vanes are built up and dressed back to profile. Cracked vanes and shrouds are welded or, on cast iron impellers, cold-repaired by metal stitching where heat would distort the part. Worn wear ring surfaces, hub bores and keyways are machined or sleeved back to size. The impeller is then checked for concentricity and balance before it goes back on the shaft. Cast iron, bronze and stainless steel are all welded in-house.
New impellers, including obsolete patterns
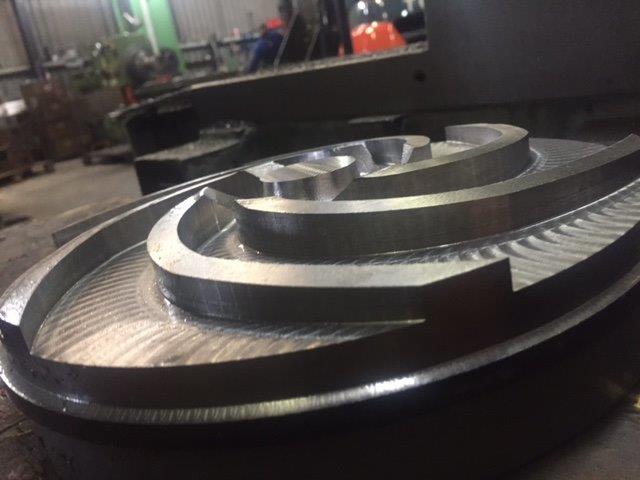
When an impeller is beyond repair or no longer available, CRS Group manufactures a replacement. A worn sample is measured and modelled, the vane geometry is reconstructed, and the new part is cast and machined to the original dimensions. CRS Group’s 3D scanning and CAD/CAE division can capture complex vane profiles directly from the old part where a drawing does not exist. This is the same component manufacture capability CRS Group uses for con-rods, camshafts and crankshafts, applied to pump parts.
Material is matched to the duty: grey or ductile cast iron for general water and process service, bronze for seawater and corrosive duties, stainless steel for chemical, food and high-wear applications.
Casings and the rest of the pump
Impeller work is usually done alongside the casing. CRS Group repairs cracked cast iron pump housings by metal stitching, rebuilds eroded volutes by welding, and machines wear ring seats, bearing landings and flange faces back to size. Restoring both halves of a worn pair gets the pump back to its design clearances and efficiency, rather than fitting a new impeller into a worn casing.
Every job is quoted on the impeller size, material, damage and whether it is a repair or a new manufacture. Photos, the pump make and model, and the sample part are enough to start. Lead time is given realistically at quote stage based on current workshop load.
Experience
- Repeat impeller manufacture and cast iron pump housing repair for a Durban refinery
- Pump and process plant work for sugar mills and agricultural processors in KwaZulu-Natal
- Slurry and dewatering pump components for mining and quarrying
- Marine and port equipment in Durban harbour
- Full member of the Metal Industries Association and the Durban Chamber of Commerce and Industry
Related services
- Component manufacture
- Specialised welding in cast iron, bronze, stainless and aluminium
- General engineering: bores, landings, keyways and faces
- 3D scanning and reverse engineering for parts without drawings
- Metal stitching for cracked cast iron casings
Get a quote on an impeller
Send photos and the pump details, or drop the worn impeller at the Mayville workshop, and CRS Group will advise whether to repair, re-machine or manufacture new.
Phone: 031 209 3168
WhatsApp: 084 511 5929
Email: info@crsgroup.co.za
Workshop: 16 Saxon Avenue, Mayville, Durban, 4058